- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
Forged vs Cast Carbon Steel Pipe Flange: Why Forging Wins for Load-Bearing Joints
Oct 7 2026
Carbon Steel Pipe Flange is almost always forged rather than cast for load-bearing joints, because the forged grain follows the stress and the part is denser, while a casting can hide a void. We explain the trade and when a casting is acceptable. In this piece we compare the two and show how we at Xi'an QinSteel forge them.
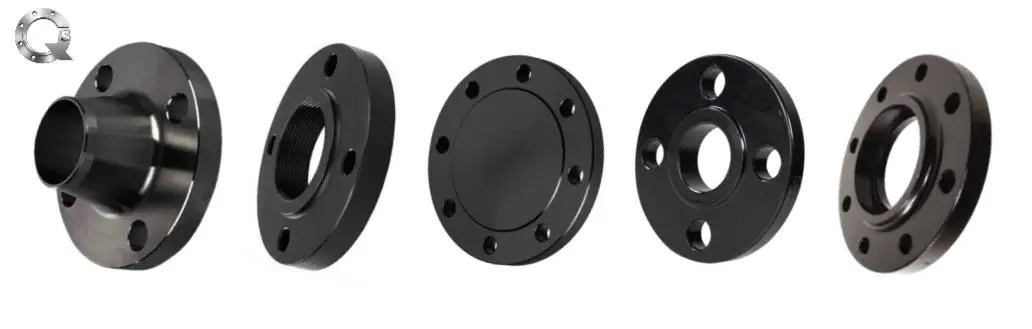
The Grain Is the Difference
Carbon Steel Pipe Flange in forging, where the steel is pressed so the grain runs along the hub and the bore, taking the load. Casting pours into a mould with a random grain and possible shrinkage. We forge the load-bearing sizes so the grain is right.
A buyer's cast blank cracked at the hub under a hydrotest; our forged replacement passed without a question.
Density and Voids
Carbon Steel Pipe Flange favour forging, because a casting can hide a shrinkage void that only shows at pressure. We forge to avoid that risk on the joints that matter. A void at the bore is a leak at startup.
We forge rather than cast the weld necks so the bore is sound, not a lottery.
Cost Tilts to Cast for Huge Sizes
Carbon Steel Pipe Flange where a forge is uneconomic, and a casting may be the only route above a certain diameter. We tell the buyer when casting is the honest choice. A forced forge on a huge blank is a cost spike.
Above a certain size we discuss casting with the buyer so the price is real, not assumed.
When Casting Is Acceptable
carbon steel pipe flanges is for low-stress, low-pressure blanks and spacers where the load is light. We still certify the cast part and inspect it. A casting on a high-stress joint is a risk we flag.
We cast only the low-duty blanks and tag them so the store knows the limit.
Traceability Applies to Both
carbon steel flange with the heat stamped and 3.1 issued, but forging gives the cleaner NDE story. We certify whichever route and note it. A part with no traceability is a query at audit.
We keep the heat-to-cert link tight so a single number traces the forge or the cast.
Tagging by Route
CS pipe flange matters because a forged and a cast blank can look alike. We stamp the route on the pad. A blank with no tag is a mystery at turnaround.
We colour-tag the forge route on mixed orders so goods-in sorts by eye before reading the stamp.
Bolting, Gaskets and Joint Fit-Up
Bolting matters as much as the disc: we confirm the stud length and the gasket type so the joint is complete on arrival. A carbon steel flange that ships without the right studs is half a joint, and the fitter ends up hunting a thread across three crates.
A sample-first approach suits a new standard or a new buyer: we cut one carbon steel part, ship it, and confirm it bolts before the balance is released. A trial piece is cheaper than a container of near-misses, and it settles the dimension question for good.
Certification, Traceability and Goods-In Checks
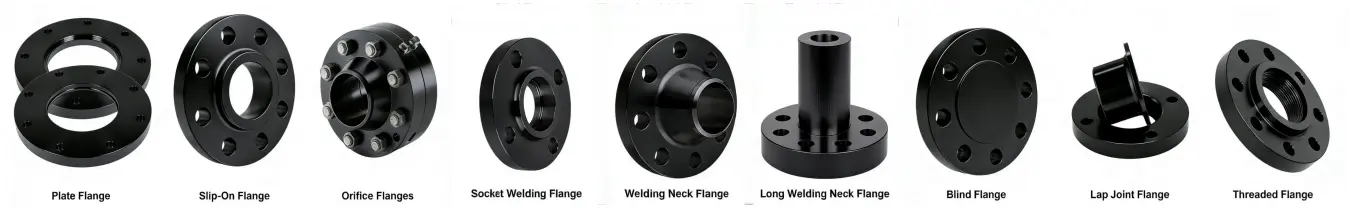
We stamp the heat on the pad and issue 3.1 on request, so your quality record traces the steel back to the melt. A part that cannot be traced is a liability at audit, and the stamp plus cert is the line that keeps a project moving.
For sour or cold duty we confirm the NACE level or the impact temperature before we forge, because the grade is decided upstream of the machine. A carbon steel part that misses the test is a failure mode, not a cost saving, and we certify it up front.
For export we handle the commercial invoice, the packing list, and the mill cert in one pack so Customs and your goods-in get the same story. A carbon steel shipment with mismatched papers is a hold, and the aligned documents are the step that clears the port.
Packing, Coating and Export Logistics
Crating protects the machined face, and we photograph the pack so condition is visible before shipping.
Logistics for export matter as much as the steel. We crate to survive a container, a crane, and a Customs hold, and we photograph the pack so you can see the condition before it sails. A carbon steel part that stains in transit is a rejected part, not a saving.
Coating the machined face before it leaves the bay is the cheap insurance against a stain that weeps on the first reopen. A carbon steel face that arrives bare in a coastal store is a rejected part, and a quick coat on the line costs less than the rework call.
Storage at the destination decides whether the coat survives, so we wrap the machined face and tag the crate for the store. A part that rusts on a humid rack is a write-off, and the wrap plus tag is the step that keeps it clean until the weld.
Communication during the build is part of the product: we send a photo of the pack and a copy of the cert so you see the part before it sails. A buyer who can see the condition avoids the dispute, and the photo is the proof that earns the trust.
For offshore or remote sites we crate to the lift plan and mark the unit mass so the crane is sized before arrival, not after a failed lift. A carbon steel part that surprises the crew on a platform is a delay no one budgets for.
We photograph the finished part and the pack so the condition is visible at every handover, from our bay to your store. A carbon steel disc that arrives with a dent has a photo to answer the question of where it happened, and that ends the argument.
The crane and the crate are part of the delivery: we size both to the part so it arrives in one piece. A carbon steel disc dropped in handling is a lost day and a re-order, and the plan that prevents it is written before the steel moves.
Stock, Repeat Orders and Phased Release
On a phased build we release flanges in lots against your install dates, which keeps cash free and the yard honest. A buyer who takes a full container of spares ties up money on parts he may not use for a year, and the release plan avoids that trap.
For a one-off diameter we quote from plate and confirm the delivery window before you commit, because a vague lead time is worse than an honest long one. A carbon steel disc cut from plate is only as good as the window we give you to plan the weld.
We hold common sizes on the shelf and cut the odd ones from plate, so the long pole is rarely the flange. A carbon steel part pulled from stock ships in days, while a cut one is quoted honestly with a window you can plan around.
We keep the drilling template for the common standards so every repeat order is cut to the same circle, not a fresh guess. A carbon steel part that matches the last one is the part your fitter expects, and consistency is what keeps a store honest.
How We Confirm the Specification Before We Cut
Email info@sxqinsteel.com with the duty and size and we return a confirmation the same business day. For large cast we confirm the route.
The documentation pack we send names the standard, the class, the facing, and the grade in one row, so the confirmation is a single glance, not a search. We have found that a clean sheet prevents most of the field calls we used to get on mixed orders.
When you send a line list, include the mating flange class and the facing, not just the size, because the two together decide the thickness and the gasket. A missing facing is the most common cause of a part that will not seat, and we return a sheet that lists both.
We run a pre-order check that lists the standard, the class, the facing, and the grade, and we send it back before cutting so a mismatch is caught on paper, not in the field. A carbon steel order confirmed in writing is an order we can stand behind.
Tagging the isolated or the spare point so the next crew knows what it is, not just that it exists, is the small step that pays back at turnaround. A carbon steel disc with no tag is a mystery, and mysteries cost the schedule far more than the tag did.
Why Choose Xi'an QinSteel for Carbon Steel Pipe Flange
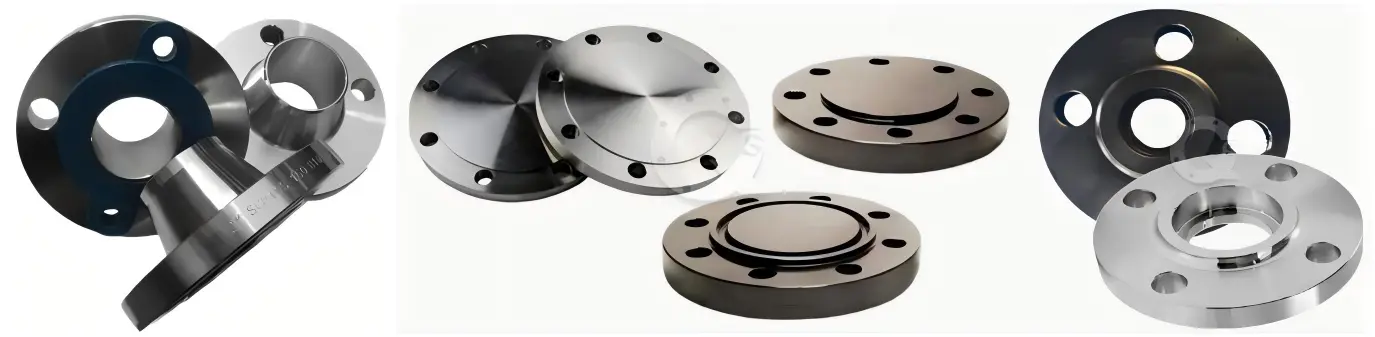
We keep common forged sizes on the shelf and forge the odd ones, releasing against your dates. A late part is a unit down.
We forge the load-bearing carbon steel flanges and cast only the low-duty blanks, certifying the route and the heat before release. Our pre-order sheet lists standard, class, grade, and forge/cast in one row. We confirm the facing groove or the RF height with a gauge rather than by eye, because a few thousandths has leaked before. A carbon steel face that is cut to the gauge seats the gasket without a torque drama, and the gauge is the check we never skip.
We match the flange wall to the pipe schedule so the joint looks right, not just the bore, because a stub that sticks out is a reface. A carbon steel part that follows the line wall seats without a shim, and the weld reads true on the radiograph. We bundle the studs, the gasket, and the disc where the job allows, so the joint is complete on arrival rather than assembled from three crates. A carbon steel set that travels together is a fitter who is not hunting a thread across the yard.
| Aspect | Forged | Cast |
|---|---|---|
| Grain | Along stress | Random |
| Voids | Rare | Possible |
| Cost small | OK | Lower |
| Cost large | High | OK |
| Use | Load | Low duty |
Frequently Asked Questions
1.Forged or cast for my joint?
Forge for load-bearing; cast only for low-duty, low-pressure blanks.
2.Is casting acceptable?
Yes for light-duty blanks and spacers, certified and inspected.
3.What proves the route?
Heat number, route stamp, and 3.1 certificate.
Contact Xi'an QinSteel for Carbon Steel Pipe Flange Solutions
For pricing and lead time on Carbon Steel Pipe Flange stock or a made-to-order run, email info@sxqinsteel.com or open www.sxqsteel.com. Send the duty, size, and class, and we forge or cast the flange with the route certified and tagged so the store knows the limit.
References
1.ASTM A105 - Carbon steel forgings for piping components.
2.ASTM A216 - Cast carbon steel for pressure service.
3.ASME B16.5 - Flange dimensions.
4.ISO 10474 / EN 10204 - Inspection documents, 3.1 certificates.
5.ASME B16.47 - Large diameter context.
6.MSS SP-44 - Steel Pipeline Flanges.
Learn about our latest products and discounts through SMS or email